
OEE is calculated after the shift, not during it
By the time downtime is visible in a report, the shift is over and the cause is a memory.
Supply chain & industry
Production runs on the floor. Reporting runs on a spreadsheet assembled the following morning.
manufacturing industry groups saw labour productivity decline over the latest published year.
Source: BLS: Productivity and Costs by Industry, Manufacturing and Mining
What is happening
By the time downtime is visible in a report, the shift is over and the cause is a memory.
Inspection results in one system, scrap in another, customer complaints in a third. The link between them is a person.
Sensors exist on newer lines. The data does not reach anyone before the failure does.
When a customer asks which batches contained a suspect lot, the answer takes days and a lot of manual searching.
Intelligence, plumbed in
The build is a machine connector, one fault vocabulary across lines, and a test set of failures you have already had.
How we make AI survive real data Connectors
 A semantic layer
 Evals you can check
What changes
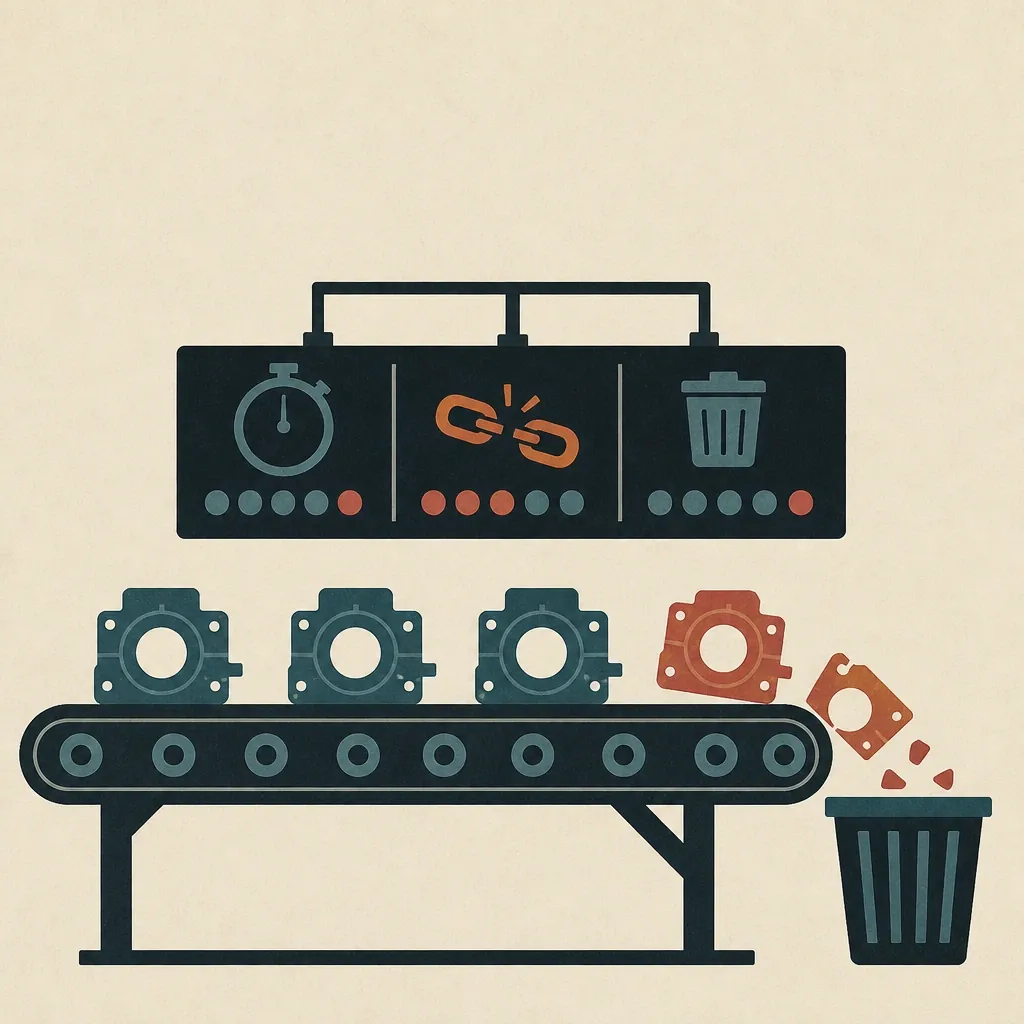 Live
Downtime, cycle time and scrap as they happen, attributed to line, shift and cause.
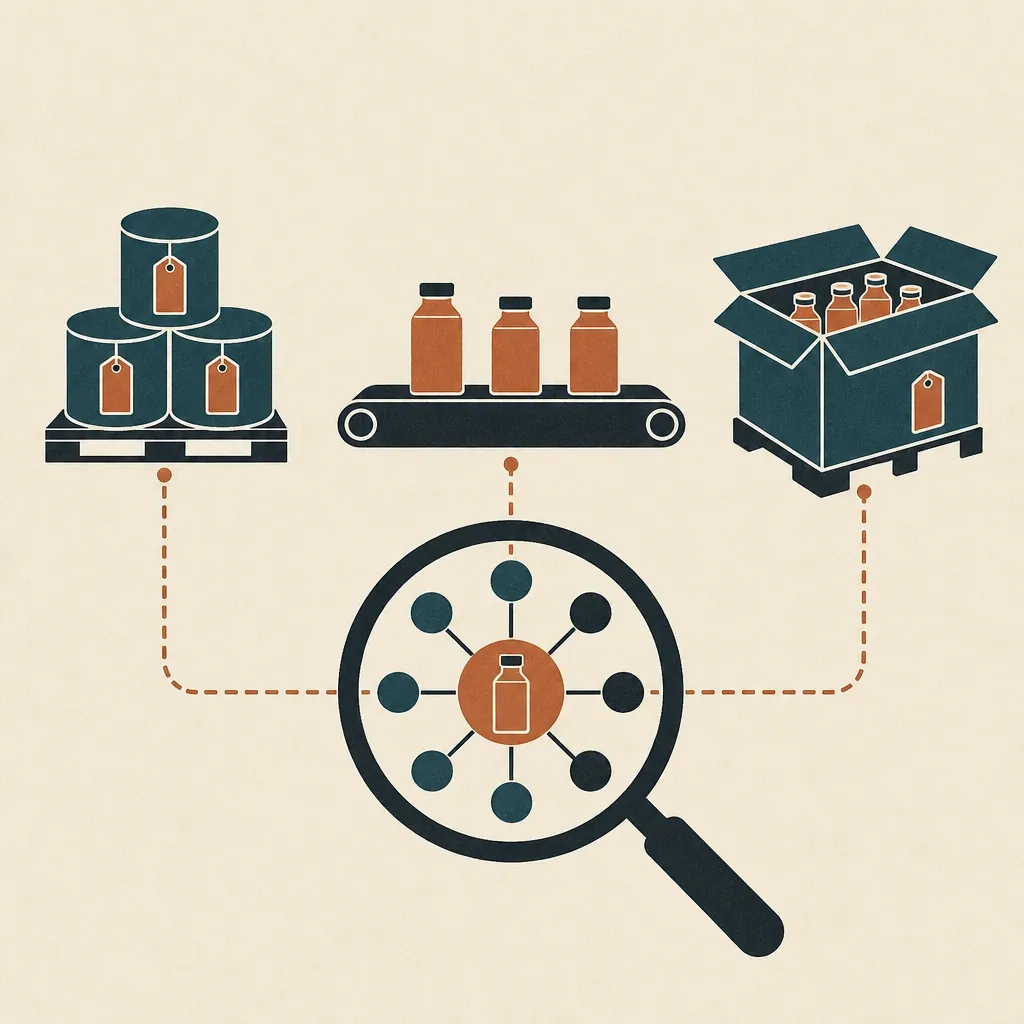 Traced
Raw lot to finished unit to customer shipment, queryable rather than reconstructed.
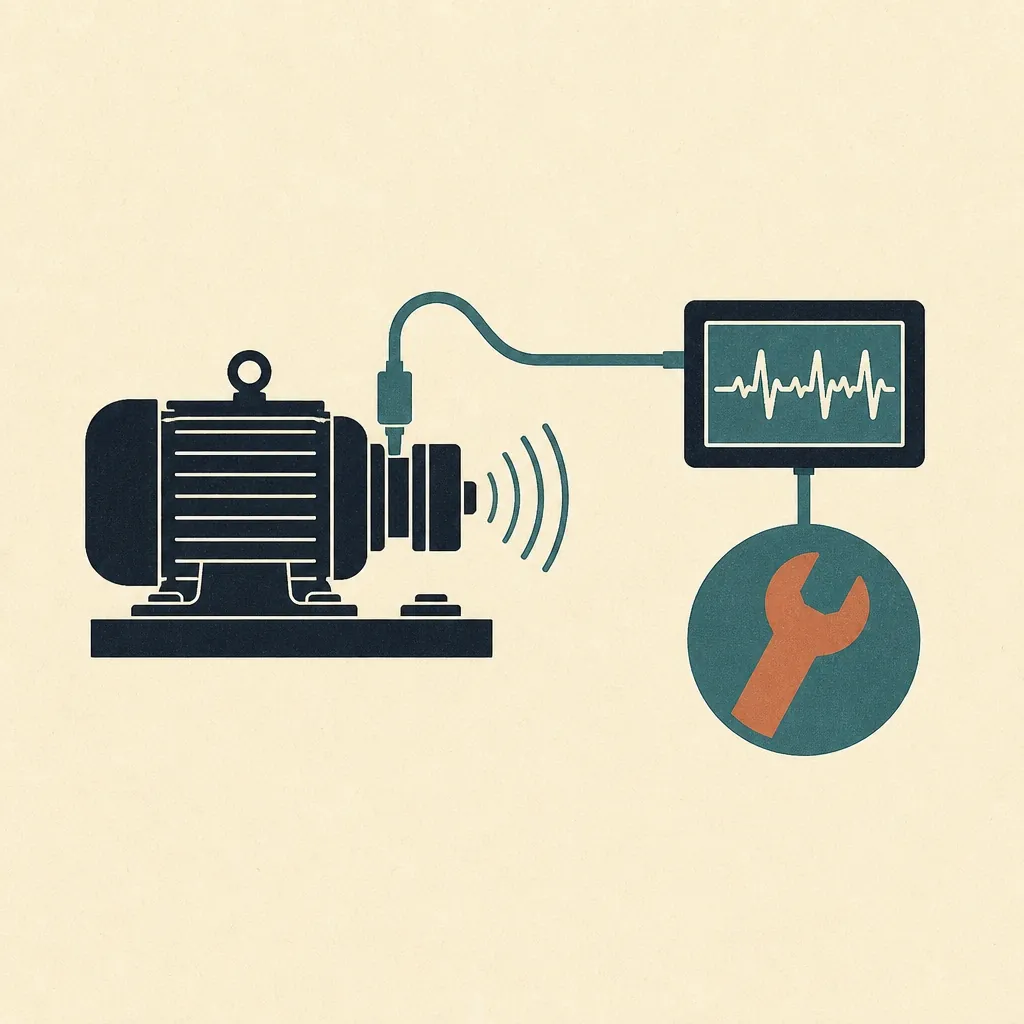 Predicted
Using the sensor data already being generated and currently discarded.
Research
Each one carries its own figures and the citations behind them. Start with whichever sounds most like your week.
Federal figures show labour productivity declining across most manufacturing industry groups. Machine data is abundant. The work between machines is not recorded at all.
United StatesContract device makers grow by buying plants. Each one arrives with its own travellers, lot numbering and record format, and the auditor still expects one traceable story.
EuropeContract furniture makers win hotel and retail projects on bespoke work. Each brief arrives as someone else's drawings, schedules and specs, and quoting waits for a person to read them all.
European UnionMakers of packing and sorting lines build each one to order, then service it for years. The real record of each line sits in service reports and engineers' notes.
EuropeGroups of contract manufacturers grow by buying local shops. Each shop still quotes from its own records, so the group never sees what it already knows.
United StatesPrecision machining groups grow by buying shops. Each shop arrives with its own machines, job history and quoting habits, and requests still land wherever the customer first sent them.
EuropePipe makers now sell complete heat-network systems. Each bid still means reading someone else's network plans and costing every run by hand, often in two separate catalogues.
However hard, whatever it is
We wrote this about the shop floor seeing what the line already knows. If yours is quality, changeover or a supplier nobody can measure, same job.
 01
Days where the work happens, not a workshop in a meeting room. We watch the job get done and write down the shortcuts nobody wrote down.
 02
Your data, your rules, your vendors and their documentation, and the published research on your sector. We report what is actually in there.
 03
Not which tool fixes this. What is actually causing it, taken apart until we reach the piece that cannot be divided further.
 04
Weeks, not quarters. By this point we are not guessing what to build, and guessing is the thing that makes projects long.
Where we sit
What you get
Built new for you — none of this exists in your stack today
What you already run — unchanged, and still yours
If the machine shows it, we can read it. If it has no port, we build one. PLC tags, OPC-UA, a panel meter with nothing but a display. And where there is nothing, a sensor we make.
 No API
 No documentation
 A terminal from 1994
 It arrives as paper
 The vendor said no
 It reports nothing
Not a list of limits. Name yours on the call.
And once we can reach it, a model can read it. Most of the value here is in the sources nobody ever structured — the note, the letter, the screen.
Who this is for
 Plant Manager
 Operations Director
 Quality Head
 Maintenance Manager
 Supply Chain Director
Straight answers
Usually, yes. Older equipment can be read through PLC interfaces, retrofitted sensors or edge devices without touching the control system. We have built embedded and sensor firmware as well as the software above it, which matters when the answer is 'it depends on the machine'.
No. We read from them and build the operational layer above, which is faster to deploy and does not put production at risk.
Carefully and with your controls engineers. Read-only wherever possible, segmented from the control network, and never a component that production depends on to run.
Yes. The log and the fault code describe the same event. We test against failures you have already had before the floor relies on it.
Also in supply chain & industry
Stockouts and excess inventory persist in organisations that bought every system designed to prevent them.
Supply chain & industryAnd the average project still overruns by twenty-eight percent.
Supply chain & industryWhich is why the operation stays reactive when the data to be proactive already exists.
Next step
20 minutes. Free.
You tell us what is not working. We ask how the work really gets done.
A few weeks.
We read your systems, including the notes and letters no field holds. You get what is really in there, what it costs, and the accuracy we can hit.
A few months.
Only if step 2 says it is worth it. Fixed price, agreed before we start.